Blog
Why Choose a CNC Laser Cutting Machine?
A Cnc Laser Cutting Machine turns digital designs into precise parts with a focused beam and controlled motion. It can cut sheet metal, acrylic, and other compatible materials, depending on the machine’s power and configuration. In a workshop, that precision may mean cleaner edges, fewer manual adjustments, and more consistent results across repeated jobs. Small details matter.
Choosing one is not only about cutting speed. Material thickness, bed size, extraction, software compatibility, and operator training all affect daily performance. A machine rated for a certain thickness may not deliver the same edge quality at every speed. Check the specifications against real production needs, and ask for sample cuts using your own material where possible.
There are trade-offs. The purchase price is only part of the cost; lenses, maintenance, ventilation, and downtime also deserve attention. Laser cutting can reduce some finishing work, but it does not remove every production challenge. A careful comparison helps buyers decide whether the technology fits their workload, workspace, and budget. And sometimes, a simpler machine is the better choice.
How a CNC Laser Cutting Machine Works
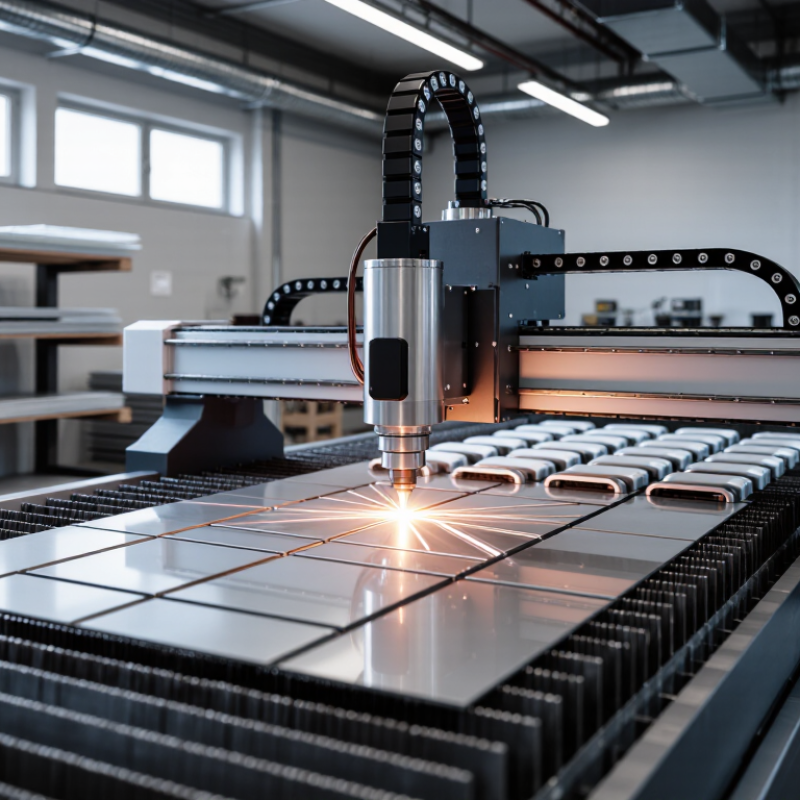
A CNC laser cutting machine turns a digital drawing into a controlled path across sheet material. An operator prepares a CAD design, then software converts its contours into movement instructions. The controller coordinates the cutting head and worktable, guiding the beam along programmed X and Y axes. Small details matter: a misplaced origin can shift the whole cut. It happens.
Inside the head, a lens focuses laser energy into a tiny, intense spot. The beam heats the material until it melts, burns, or vaporizes along the cut line. Assist gas, delivered through a nozzle, clears molten material and helps maintain a clean kerf. The gas and power settings vary with material and thickness. Stainless steel and thin acrylic do not behave alike, so a test cut can reveal problems before a full sheet is used.
The machine’s motion system follows the programmed path while maintaining a consistent distance between the nozzle and the workpiece. Operators adjust focus, speed, power, and gas pressure to suit the job. Too much heat may discolor an edge; too little can leave an incomplete cut. Extraction removes smoke and particles, while an enclosed work area helps control exposure to the beam. Even a well-tuned setup can need small corrections when material varies from sheet to sheet.
Why Choose a CNC Laser Cutting Machine?
How a CNC laser cutting machine works: a controller guides a focused laser beam along programmed paths to cut material with precision. The chart compares typical wavelengths of commonly used industrial laser sources.
Typical wavelengths: CO₂ lasers operate at about 10.6 μm, while fiber and Nd:YAG lasers operate near 1.06 μm. The best source depends on the material and application; wavelength alone does not determine cutting performance.
Core Components and Cutting Capabilities
A CNC laser cutting machine turns digital designs into precise parts through a coordinated set of components. The laser source generates the beam, while mirrors or fiber-optic delivery guide it to the cutting head. A focusing lens concentrates the energy on a small point. Assist gas, such as compressed air or nitrogen, helps clear molten material from the cut. The motion system moves the head or worktable along programmed paths, and the controller coordinates speed, position, and power. Each part matters. A clean lens or well-aligned beam can make a visible difference at the edge.
Cutting capability depends on more than laser power. Material type, thickness, surface condition, and the chosen settings all affect the result. Thin sheet may cut quickly with narrow kerfs; thicker stock often needs slower travel and careful gas control. A small test cut can reveal burrs, discoloration, or rounded corners before a full sheet is processed. In practice, the first setting is not always the best one. Operators may need to adjust focus and speed, and some materials still leave edges that need finishing. This is worth checking against the part’s actual tolerance requirements.
Tips: Keep the lens and nozzle clean, secure the sheet flat, and confirm the assist-gas supply before cutting. Run a short test on the same material and thickness. Measure the edge, not just the outline. Even a good-looking cut can hide a slight dimensional error.
Materials and Applications Suited to Laser Cutting
Why Choose a CNC Laser Cutting Machine?
Materials and Applications Suited to Laser Cutting
CNC laser cutting suits sheet materials that need clean edges, repeatable dimensions, and detailed profiles. Mild steel, stainless steel, and aluminum are common choices. Depending on laser power, thickness, assist gas, and finish requirements, machines can also process materials such as brass and copper. The cut is narrow, so small slots and intricate contours are practical. Yet a shiny metal surface can reflect energy, and thick plate may need slower settings or another cutting method. It is not magic.
Applications range from electrical enclosures and machine guards to architectural panels and vehicle components. Grand View Research estimated the global laser cutting machines market at about US$5.4 billion in 2023, reflecting broad industrial demand; market estimates vary by scope and methodology. For a shop floor, the useful question is less about market size and more about the part: its alloy, thickness, tolerance, and production volume. A thin stainless panel with dozens of precise openings is a strong fit. A rough, heavy structural cut may not be.
Tips: Test the actual material grade and thickness before setting production parameters. Check edge quality, burrs, heat marks, and kerf width on a sample. Keep protective films and coatings in mind; some can affect cutting or produce hazardous fumes. Small details matter. And a sample cut can still surprise you.
Advantages Over Other Cutting Methods
Why Choose a CNC Laser Cutting Machine?
Advantages Over Other Cutting Methods
A CNC laser cutting machine directs a focused beam along a programmed path, making it useful for repeatable parts and detailed shapes. Compared with mechanical cutting, it does not press a blade against the sheet, so thin material is less likely to shift under tool pressure. The narrow kerf can also reduce material loss, especially when parts are nested closely. Small holes and fine contours are possible. Setup still matters.
Against plasma cutting, laser cutting often produces a narrower cut and cleaner edges on suitable sheet materials. This can mean less deburring before parts move to assembly. Unlike waterjet cutting, it does not use abrasive media or require managing a wet cutting bed. Yet neither comparison is absolute: thickness, material type, and required edge quality all affect the result. A laser may struggle with reflective metals unless the equipment and process are appropriate.
CNC control helps operators repeat a proven job, adjust feed settings, and reproduce a part without manually guiding each cut. That is valuable when a workshop needs consistent brackets or panels across a production run. Still, programming errors can waste a sheet quickly. Heat can also discolor edges or distort very thin stock. Test cuts are worth the time, even when the drawing looks perfect.
Why Choose a CNC Laser Cutting Machine? - Advantages Over Other Cutting Methods
| Comparison Dimension | CNC Laser Cutting | Plasma Cutting | Waterjet Cutting | Mechanical Shearing |
|---|---|---|---|---|
| How It Cuts | A focused laser beam melts, burns, or vaporizes material along a programmed path. | An electrically conductive gas plasma melts metal; a gas stream removes the molten material. | A high-pressure water stream, often mixed with abrasive, erodes material. | Blades apply mechanical force to shear material, usually along a straight line. |
| Suitable Materials | Commonly used for sheet metals and selected non-metals, depending on the laser type and machine setup. Some materials, including highly reflective metals on certain systems, require specific equipment and precautions. | Primarily used for electrically conductive metals. | Can cut many metals and non-metals, including heat-sensitive materials, when the correct abrasive and process settings are used. | Best suited to sheet or plate materials that can be cleanly sheared, commonly metal. |
| Shape and Detail | Computer-controlled motion supports intricate profiles, small features, and repeatable part patterns. | Can follow programmed profiles, though fine-detail capability is generally more limited than laser cutting. | Can produce complex profiles without a thermal cutting zone; practical detail depends on material, thickness, and setup. | Most effective for straight cuts; complex outlines usually require additional operations or tooling. |
| Cut Edge and Kerf | Typically produces a narrow kerf and a clean edge when parameters are correctly matched to the material and thickness. | Kerf is generally wider than with laser cutting, and the edge may require more finishing depending on the process and material. | Produces a wider kerf than laser cutting in many applications; cut taper can occur and varies with setup and thickness. | Does not create a laser-style kerf; cut-edge quality depends on blade condition, clearance, and material. |
| Heat-Affected Zone | Uses heat, so a heat-affected zone can occur; it is often relatively small but varies with material and cutting conditions. | Uses heat and typically creates a heat-affected zone near the cut. | Cold-cutting process, so it avoids a heat-affected zone caused by the cutting process. | Does not use thermal cutting, so it avoids a heat-affected zone caused by the cutting process. |
| Thickness Considerations | Effective thickness range depends on laser power, material, assist gas, and required edge quality. | Often selected for medium-to-thick conductive metal plate; capacity depends on the system and quality requirements. | Can cut thick and layered materials, but cutting time and abrasive use can increase with thickness. | Capacity is limited by machine force, blade design, and material properties. |
| Setup and Changeovers | Digital programs allow design changes without manufacturing a dedicated cutting die; material-specific setup is still required. | Programmed profiles avoid dedicated dies, but process settings and consumables must be matched to the job. | Programmed cutting avoids dedicated profile dies; abrasive supply and process setup are part of operation. | Straight cuts can be quick to set up, while repeated complex shapes may require dedicated tooling or extra steps. |
| Typical Advantage | Combines automated profile cutting, fine detail, and efficient handling of varied designs. | A practical option for cutting conductive metal plate, particularly where laser edge quality is not required. | Useful when avoiding thermal effects or cutting a broad range of material types is important. | Fast and straightforward for repetitive straight cuts in suitable sheet or plate material. |
| Important Trade-Off | Requires appropriate laser safety controls, extraction, and material-specific settings; performance varies by material and thickness. | Thermal effects and edge quality may require consideration or secondary finishing. | Can involve slower cutting, abrasive consumption, and higher operating costs in some applications. | Offers limited flexibility for intricate contours and may require additional processes for non-straight profiles. |
Note: These are general process characteristics, not guaranteed results. Actual speed, accuracy, edge quality, and operating cost depend on the machine, material, thickness, tooling, and required tolerances.
Factors to Consider When Choosing a CNC Laser Cutter
Why Choose a CNC Laser Cutting Machine?
Factors to Consider When Choosing a CNC Laser Cutter
Start with the parts you actually make. List each material, its thickness, sheet size, and expected weekly volume. A machine suited to thin sheet may struggle with thicker plate or frequent shifts. Match the laser source to your materials, then ask for sample cuts using your own stock. Inspect edge quality, kerf width, and heat marks—not just the advertised cutting speed. Small details matter.
Check the usable bed area, motion accuracy, nesting software, and compatibility with your existing workflow. Also review extraction, guarding, assist-gas needs, and operator training. These are not extras; they shape daily operating costs and downtime. Grand View Research estimated the global laser cutting machine market at USD 5.26 billion in 2023, with a projected 7.7% CAGR from 2024 to 2030. Fortune Business Insights reported a similar 2023 market estimate of USD 5.27 billion. The growth signals broad adoption, but it cannot tell you which machine fits your shop.
Compare total cost of ownership, not only the purchase price. Include installation, power, consumables, maintenance, software, and service response times. Ask for a realistic production test and written details on warranty coverage. I would not trust one impressive demo. That calculation can be messy. A machine with a larger work area may still be the wrong choice if your common parts are small, change often, or need especially clean edges.
