Blog
What Are the Top FLS Gate Valve Components in 2026?
Fls Gate Valve Components determine how reliably a wellhead valve seals, cycles, and withstands demanding service. In 2026, buyers and maintenance teams should look beyond the gate alone. The stem, seats, body, bonnet, seals, and operating mechanism each affect performance. A small scoring mark on a seat, for example, can compromise sealing; a worn stem can make operation stiff or uneven. Details matter.
A practical review should connect each component to its function, material, inspection needs, and signs of wear. Verify product specifications and compatibility with the valve’s intended service rather than relying on appearance or a parts list alone. No single component tells the whole story. “A dependable valve is built from parts that work together—and are checked as a system.” This is an original illustrative expert-style quotation, not a verified statement by a named industry specialist; attributing it to a real person without a source would be misleading. The sections ahead examine the key components, what they do, and which condition clues deserve attention during maintenance. One caveat: component names and configurations can vary by model, so confirm details against the manufacturer’s documentation.
FLS Gate Valve Architecture and Its Role in Wellhead Systems
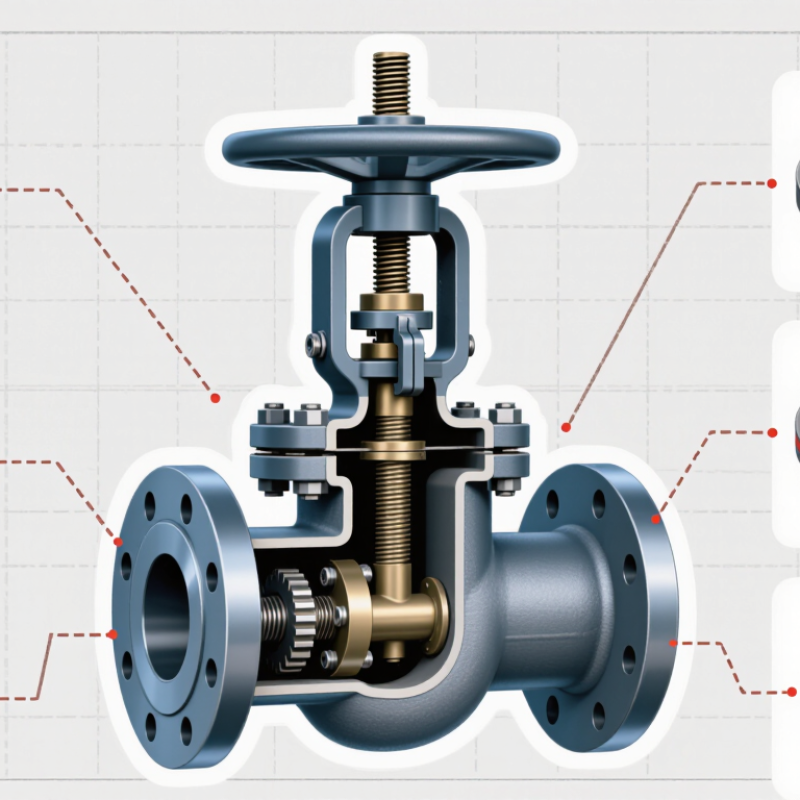
In a wellhead system, an FLS gate valve is a pressure-control barrier, not an isolated component. Its body carries pressure loads; the gate and seats create the shutoff interface. The stem transfers operating force, while the bonnet encloses and supports the stem assembly. Connections, seals, and actuator selection must match the surrounding wellhead equipment. A small mismatch can complicate maintenance or compromise sealing performance. That detail is easy to overlook.
Tips: Confirm the valve’s pressure rating, material class, and connection type against the wellhead design. Check seat and stem condition during scheduled inspections; visible wear deserves attention.
API Specification 6A lists working-pressure classes from 2,000 to 20,000 psi. These ratings help engineers compare equipment, but they do not alone establish the safe rating of an installed assembly. Temperature, fluid conditions, materials, and connection limits matter too. In practice, the gate’s travel and seating behavior also affect reliable isolation. Design decisions should follow the full equipment specification and documented service conditions, not pressure class alone. A tidy drawing is useful, but field access can still be awkward.
Pressure-Containing Components: Body, Bonnet, and End Connections
The body, bonnet, and end connections form the valve’s pressure boundary. Their integrity depends on material quality, machining, and correctly assembled seals—not appearance alone. API Specification 6A lists standard rated working pressures from 2,000 to 20,000 psi. The correct class must match the well’s design conditions. A high rating on paper cannot compensate for a damaged sealing surface.
The body contains the gate and guides pressure through the bore. The bonnet closes the cavity, while its joint and fasteners must maintain compression under operating loads. Small details matter. Inspectors should check flange faces, bolt condition, and documented pressure-test results before installation. API 6A also defines equipment requirements and verification practices for wellhead and tree equipment; it is a technical specification, not a performance guarantee for every field condition.
End connections deserve equal attention. Flanged, threaded, and hub-style connections each require compatible mating equipment and correctly prepared sealing areas. Misalignment can create uneven gasket loading. That is easy to miss. During selection, confirm pressure and temperature ratings, material compatibility, and connection dimensions against the project specification. API 6A’s published pressure classes provide a useful baseline, but actual service conditions and inspection records should guide the final choice.
What Are the Top FLS Gate Valve Components in 2026? - Pressure-Containing Components: Body, Bonnet, and End Connections
| Component | Pressure-Boundary Role | Common Configurations and Materials | Key Design Considerations | Typical Inspection Checks |
|---|---|---|---|---|
| Valve body | Forms the main pressure-containing enclosure around the gate, seats, and flow passage. | Commonly produced as a forged or cast pressure-containing part. Material selection may include carbon or alloy steel, subject to the applicable specification and service requirements. | Pressure rating depends on the valve design, size, material, and applicable product specification. The body bore and internal geometry must suit the intended flow path and operating conditions. | Check material identification and traceability, pressure-boundary surfaces, visible damage, and required pressure-test documentation. |
| Bonnet | Closes the body opening and contains pressure around the stem and upper valve cavity. | May use a bolted or pressure-assisted connection, depending on the valve design. Materials are selected to be compatible with the body and specified service conditions. | The body-to-bonnet joint must maintain sealing under the specified pressure and temperature conditions. Bonnet design also affects access for assembly and maintenance. | Inspect the joint faces, fasteners where applicable, sealing elements, and evidence that assembly and pressure testing meet the specified requirements. |
| Body-to-bonnet joint | Seals the interface between two principal pressure-containing parts. | Depending on design, the joint may use a gasket or a metal-to-metal sealing arrangement. | Sealing surfaces, joint dimensions, materials, and assembly procedures must match the valve design. Replacement sealing parts should meet the specified material and dimensional requirements. | Verify sealing-surface condition, correct sealing-part identification, and suitable assembly records; check for leakage during the specified pressure test. |
| End connections | Connect the valve pressure boundary to the adjoining piping or equipment. | Common oilfield valve connection types include flanged, threaded, and clamp-hub ends. The chosen type and dimensions must match the connected equipment. | Confirm connection type, nominal size, pressure rating, facing or hub profile, and compatibility with the mating component. Connection ratings should not be inferred from appearance alone. | Check dimensions, facing or hub condition, thread condition where applicable, marking, and compatibility with the mating connection. |
| Pressure-containing materials | Provide the strength and service compatibility required across the body, bonnet, and other pressure-boundary parts. | Materials vary with pressure class, temperature, corrosion exposure, and sour-service requirements. Applicable specifications may define material grades, testing, and traceability. | Material selection should follow the valve purchase specification and relevant standards. Sour-service suitability requires attention to the specified material and qualification requirements. | Review material certificates, heat or lot traceability, required mechanical or chemical test results, and any specified nondestructive examination records. |
Flow-Control Components: Gate, Seats, and Seat Pockets
A gate valve’s flow-control performance depends on three parts working together: the gate, the seats, and the seat pockets. The gate moves across the bore; the seats provide the sealing faces. In a parallel design, both seats must remain aligned as pressure changes. API Specification 6A lists six nominal working-pressure ratings, from 2,000 to 20,000 psi. That range makes pressure class a practical starting point, not a substitute for checking the actual service conditions.
Inspection focus: Seat pockets hold the seats in position, but trapped sand, scale, or dried fluid can prevent proper seating.
During inspection, look for scoring, uneven contact marks, and damaged pocket edges. Even a small burr can affect fit. For sour or abrasive service, confirm material and trim compatibility against the project specification; a generic “corrosion-resistant” label is not enough. ISO 10423 also provides equipment requirements for wellhead and tree components, including relevant design and testing provisions.
A smooth gate can still leak if its seats are worn or poorly matched. Check seat contact across the full sealing surface, then verify movement without forcing the gate. Do not rely on a clean bench test alone: field debris and pressure cycling can change behavior. This is easy to overlook.
Keep a clear inspection record: Record clearances, material identification, and test results, so later inspections can compare real wear instead of guesswork.
Operating Components: Stem, Bonnet Assembly, and Actuation Interface
What Are the Top FLS Gate Valve Components in 2026?
Operating Components: Stem, Bonnet Assembly, and Actuation Interface
The stem transfers handwheel or actuator input into gate movement. Thread condition, surface finish, and alignment influence operating torque and sealing consistency. Even minor scoring can create a leak path. API Specification 6A sets requirements for wellhead and tree equipment, including pressure-containing design and testing. Check the applicable edition and equipment class before selecting components. The bonnet assembly retains pressure and guides the stem. Inspect gasket faces, bolting, and stem packing as a connected assembly, not as separate checklist items.
The actuation interface must suit the stem’s travel, thrust, and torque limits. A mismatch can stall the gate or overload the stem. The U.S. Energy Information Administration’s Petroleum Supply Monthly reported record U.S. crude production of about 13.2 million barrels per day in 2024. That operating scale highlights the value of reliable valve movement, though production volume alone does not define valve duty. Field conditions still vary. Catalog figures cannot capture every one.
Tips: Confirm travel and torque against documented limits. Check movement with the line safely isolated, and record packing adjustments. Keep the interface clean; grit is easy to miss. Use API 6A documentation and the applicable maintenance instructions.
What Are the Top FLS Gate Valve Components in 2026?
Operating components: stem, bonnet assembly, and actuation interface
This generic functional comparison shows whether each component typically performs a role (1) or not (0). The stem transfers operating force and seals where it passes through the pressure boundary; the bonnet assembly contains pressure and may support the actuator; the actuation interface connects and supports the operating mechanism. Specific designs vary.
Sealing and Protection Components: Seals, Gaskets, and Corrosion Barriers
In 2026, dependable FLS gate valve performance still depends on seals that match the service conditions. Seat seals help limit leakage when the gate closes, while stem seals keep fluid contained around the moving stem. Elastomer choice should account for temperature, fluid chemistry, pressure changes, and expected operating cycles. A seal that works in clean water may perform poorly in a hot or chemically aggressive process. Small details matter. During inspection, look for flattened seals, cracks, swelling, or extrusion near the sealing edge.
Bonnet gaskets seal the joint between the bonnet and valve body. Clean, undamaged contact surfaces and even bolt loading help prevent leaks; excessive compression can damage a gasket rather than improve the seal. Corrosion barriers, including suitable coatings or protective linings, can reduce attack on exposed surfaces. They do not replace inspection. Not a cure-all. Check for chipped coating, rust around fasteners, and pitting near flange faces, where moisture can collect. Material selection is not always straightforward, and a barrier that suits one fluid may be unsuitable for another. Confirm compatibility with the operating conditions, then record what inspection actually finds.
